Aluminum welding is no longer a niche fabrication skill. It supports vehicle structures, rail equipment, heat exchangers, and lightweight industrial frames. The International Energy Agency reported nearly 14 million electric car sales in 2023. That growth increases demand for reliable aluminum joining. It also exposes weak process control. Thin panels can burn through quickly. Thick sections may trap porosity or develop incomplete fusion. Small changes matter.
This article examines How to optimize welding parameters for aluminum alloys through practical, measurable controls. Welding engineers commonly adjust current, voltage, travel speed, shielding gas, wire feed rate, and torch angle. AWS D1.2/D1.2M provides established guidance for structural aluminum welding. ISO 3834 adds quality requirements for fusion-welding processes. These references support a disciplined approach, but they do not replace production trials. Every alloy, joint design, and machine behaves differently.
The Aluminum Association and International Aluminium Institute both emphasize aluminum’s expanding role in transportation and sustainable manufacturing. Yet, efficiency cannot be judged by speed alone. A faster weld may create more rework, distortion, or rejected parts. In practice, a clean oxide layer, stable arc, and controlled heat input often matter more than impressive amperage. Operators should record bead appearance, penetration, defect rates, and interpass temperature. Simple records reveal patterns.
Some recommendations may need revision. No universal parameter table fits every workshop. That is the uncomfortable truth. Experienced teams validate settings on representative coupons, inspect results, and refine the procedure before production begins. Reliability comes from evidence, not guesswork.
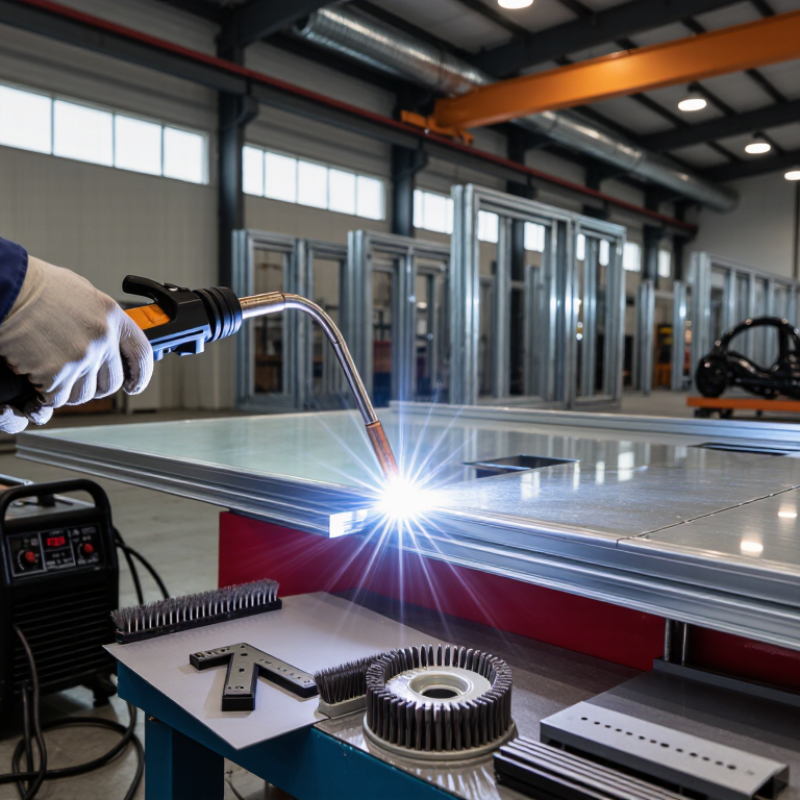
What Is the Best Way to Optimize Aluminum Welding?
Before welding aluminum, identify the alloy, temper, and joint type. Alloy markings, material certificates, and hardness checks can prevent costly assumptions. A 5xxx alloy behaves differently from a heat-treatable 6xxx alloy. The temper also matters. Welding may soften the heat-affected zone, especially in strengthened 6xxx materials. That strength may not return without a qualified heat-treatment process.
Joint design controls access, penetration, and distortion. A butt joint usually needs accurate edge preparation and tight fit-up. Lap and T-joints can trap oxides or create sharp stress concentrations. Clean the surface with a suitable degreaser and a dedicated stainless-steel brush. Remove the oxide layer shortly before welding. Select filler metal for strength, cracking resistance, corrosion exposure, and service temperature. Choosing it only by tensile strength is a mistake I have seen repeated.
Tips: Record the alloy and temper before setup. Keep the arc short and stable. Use controlled heat input. Watch the edges carefully. They melt quickly. Clamp large panels, but allow some movement for expansion. Make a test coupon using the same thickness and joint design. Inspect the weld visually, then use appropriate non-destructive testing when the application requires it. A smooth bead is not proof of a sound joint. Review the procedure after each trial, because real distortion often differs from the drawing.
| Aluminum Alloy and Typical Temper | Common Joint Type | Weldability and Main Risk | Typical Filler Metal Selection | Recommended Welding Approach | Pre-Weld Preparation | Post-Weld Considerations |
|---|---|---|---|---|---|---|
| 5052-H32 | Lap, fillet, and butt joints in sheet and light plate | Generally good weldability. Excessive heat can increase distortion and reduce the strength of the heat-affected zone. | ER5356 is commonly selected for higher strength and better color matching. ER4043 may be used when lower melting temperature and improved fluidity are priorities. | Use AC GTAW for precise thin-sheet work or pulsed GMAW for production welding. Control travel speed to limit heat input. | Remove oil, paint, and oxide. Degrease first, then use a dedicated stainless-steel brush immediately before welding. Keep joint gaps uniform. | H32 strain-hardened properties are not fully restored by welding. Design the joint and allowable stress around the softened heat-affected zone. |
| 6061-T6 or 6061-T651 | Butt, corner, and fillet joints in structural components | Good general weldability, but the T6/T651 temper is substantially overaged near the weld. Cracking and distortion can occur if heat input is excessive. | ER4043 offers good fluidity and reduced cracking sensitivity. ER5356 provides higher weld strength and is often preferred when anodizing or higher tensile strength is required. | Use AC GTAW for controlled manual welding or pulsed GMAW for thicker sections. Use a short arc, adequate wire feed speed, and the lowest practical heat input. | Remove the oxide layer and contaminants. Use a clean, close-fitting joint. For thick sections, moderate preheating may help reduce thermal gradients; verify the maximum temperature in the qualified WPS. | Do not assume the welded area retains T6 strength. A qualified post-weld heat treatment may restore some properties, but it can also affect distortion and dimensional accuracy. |
| 5083-H116 or 5083-H321 | Full-penetration butt joints, fillet joints, and marine or pressure-retaining fabrications | Very good weldability and strong resistance to corrosion in marine environments. Excessive heat can reduce strength and may affect corrosion performance. | ER5183 is commonly used when high weld strength and good marine-service performance are required. ER5356 can also be suitable when permitted by the design and service environment. | Use controlled AC GTAW for root passes or pulsed GMAW for production. Maintain adequate shielding and avoid repeated reheating of completed welds. | Clean both sides of the joint, remove oxide immediately before welding, and protect the weld zone from drafts. Use fit-up control to minimize restraint and distortion. | Check the applicable design code for strength reduction, corrosion exposure, and maximum allowable interpass temperature. Avoid contamination from carbon-steel tools. |
| 2024-T3 or 2024-T351 | Highly restrained butt or fillet joints | Poor fusion-welding suitability because copper-rich composition increases hot-cracking sensitivity. It is commonly joined by mechanical fastening rather than conventional fusion welding. | There is no universal filler choice that eliminates the alloy's fusion-welding limitations. Welding should only be considered under a qualified procedure and suitable engineering approval. | Prefer mechanical fastening, adhesive bonding, or a specifically qualified specialty process. If fusion welding is unavoidable, use low restraint, strict heat-input control, and procedure qualification. | Verify alloy and temper by material certification. Do not substitute 2024 for a more weldable 2xxx or 6xxx alloy without redesign and qualification. | Expect significant loss of temper strength near the weld and evaluate fatigue, corrosion, and crack-growth performance before production use. |
| 7075-T6 or 7075-T73 | Structural butt, lap, or fillet joints | Generally unsuitable for conventional fusion welding because zinc-rich composition creates high hot-cracking risk and severe local property loss. | No standard filler selection makes ordinary fusion welding broadly acceptable for critical 7075 structures. Use a qualified alternative joining method. | Prefer mechanical fastening, friction stir welding, or another process specifically qualified for the alloy and application. | Confirm alloy, temper, thickness, and service requirements. Avoid using general-purpose aluminum welding settings without procedure qualification. | Evaluate stress-corrosion cracking, fatigue, heat-affected-zone strength, and dimensional distortion. Critical applications require documented engineering approval. |
| 6063-T5 or 6063-T6 | Corner and fillet joints in extrusions and architectural sections | Good weldability and excellent extrusion surface quality. Thin walls are sensitive to burn-through, distortion, and loss of temper. | ER4043 is commonly selected for smooth wetting and reduced cracking sensitivity. ER5356 may be selected when higher strength or improved anodized color compatibility is required. | Use low heat input, controlled torch movement, and pulsed GMAW or AC GTAW for thin sections. Support the extrusion to maintain alignment. | Clean oxide and lubricants from the extrusion surface. Use copper or heat-sink backing where appropriate, while maintaining proper joint access. | Expect softening near the weld. If appearance is important, match filler selection and surface-finishing requirements before welding. |
| Aluminum Alloy of Unknown Grade | Any joint configuration | Unknown chemistry and temper can cause cracking, poor strength, incompatible filler selection, or unexpected corrosion behavior. | Do not select filler solely by appearance. Identify the base alloy and follow a qualified filler-metal compatibility recommendation. | Pause production welding until the material is identified through certification, marking, supplier records, or suitable material analysis. | Confirm alloy, temper, thickness, surface condition, joint restraint, and required service performance. Prepare a procedure qualification when necessary. | Record the alloy, temper, filler, process, shielding gas, heat input, and inspection results for repeatable production control. |
Set amperage, voltage, and travel speed together. Slower travel increases heat input. Use short beads and planned pauses. Avoid lingering at joint starts and ends.
Excessive heat can increase distortion and reduce process control. Measure near the weld zone, not on a distant plate. Thin sheets may still move after cooling.
An infrared thermometer offers quick readings. Reflective aluminum can mislead it. Use a contact probe or temperature indicator as a cross-check. Do not trust one reading blindly.
Use balanced tack welds and firm, moderate fixturing. Distribute heat across the joint. Weld shorter sections when practical. Leave room for contraction.
Check root gaps, alignment, and tack size first. Poor fit-up can create distortion despite good temperature records. Small corrections often matter more than higher power. This part deserves honest review.
Remove oxide and oil before welding. Use dry tools reserved for aluminum. Contamination near an edge can cause hidden lack of fusion. A bright bead is not enough.
Inspect weld size, profile, undercut, overlap, cracks, crater defects, and visible porosity. Use strong lighting. Look closely at weld toes and crater ends. Measure fillet legs with a calibrated gauge.
Critical joints may need radiographic or ultrasonic testing. Surface inspection can miss internal discontinuities. Choose the method according to joint design and project requirements. Visual approval alone proves little.
Record weld location, acceptance level, equipment calibration, and inspector qualification. Keep the evidence connected to each joint. Review records, not only appearance. Good documentation still cannot repair poor workmanship.
Optimizing aluminum welding begins with identifying the alloy, temper, thickness, and joint design, since each factor affects weldability, strength, and distortion. A key step is removing the aluminum oxide layer before welding. Although aluminum melts at approximately 660°C, its oxide melts near 2,050°C, so thorough mechanical or chemical cleaning is essential for stable arc performance and proper fusion. How to optimize welding parameters for aluminum alloys depends on selecting the appropriate process, such as AC TIG or pulsed MIG, while using 100% argon shielding gas at approximately 15–20 L/min.
During welding, control heat input by adjusting current, voltage, travel speed, and pulse settings. Keep interpass temperatures below 120°C to reduce distortion, porosity, and loss of mechanical properties. Proper fixturing, balanced welding sequences, and controlled cooling can further improve dimensional accuracy. Finally, inspect the completed weld for cracks, porosity, lack of fusion, and profile defects according to AWS D1.2 and ISO 10042 acceptance criteria.
 Mobo Robot